This guide explains how Spin Automatica systems are evaluated for operational efficiency, safety, and maintenance planning. It also provides objective background on automated spinning and control logic used in industrial production, highlighting how engineers typically compare configurations and supplier capabilities without relying on unverified claims.
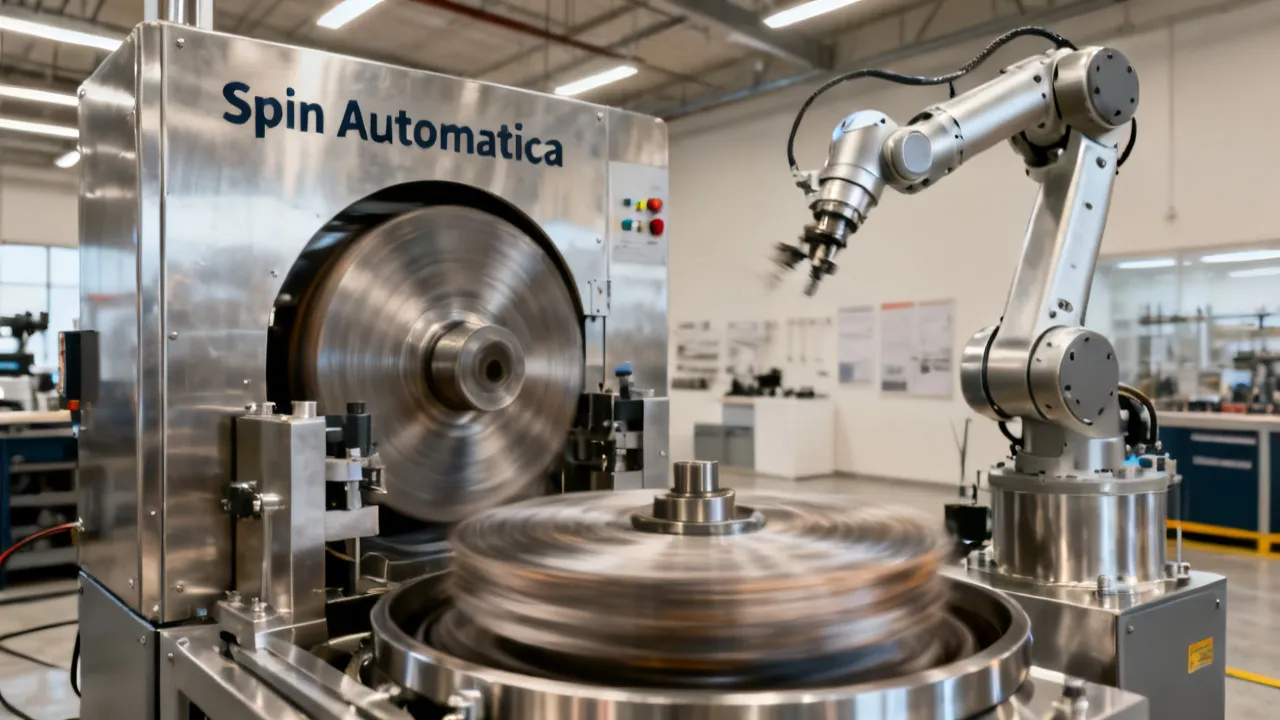
Spin Automatica is best understood as a class of industrial automation centered on controlled rotational or spinning operations—where consistency, repeatability, and safety controls directly influence throughput, quality, and uptime. In real plant environments, stakeholders typically assess Spin Automatica systems not simply on whether they “spin reliably,” but on how consistently they maintain critical process parameters over shifts, how well they integrate with existing mechanical and electrical equipment, and how quickly technicians can diagnose and resolve faults. The most valuable deployments are those that reduce variation, shorten changeovers, and preserve stable performance under real operating conditions—conditions that rarely stay perfectly ideal due to material variation, maintenance effects, operator behavior, and environmental factors.
Because each project context differs—material type, batch size, takt time, quality targets, and sometimes even regulatory constraints—this article approaches Spin Automatica with an engineering-and-procurement lens. You will see what to verify, which requirements to define before purchase, and how to compare supplier proposals using a consistent framework. That method helps decision-makers avoid hidden costs such as extended commissioning time, ambiguous service responsibilities, mismatched control interfaces that later require rework, or under-specified safety behavior that delays acceptance testing.
To keep the guidance practical, the article emphasizes evidence-based evaluation: what measurable outcomes should be required, what artifacts (test results, logs, and documentation) can prove performance claims, and what integration assumptions need to be clarified early. Throughout, the underlying theme is that Spin Automatica is not just a motor and a controller; it is an engineered system whose performance depends on closed-loop control quality, correct sensing strategy, robust safety engineering, and sound integration design.
Across industrial sectors, “spinning” or rotational forming tasks show up in multiple ways. In some processes, spinning is used to achieve coating uniformity by distributing a liquid film via rotation. In others, it supports fiber or filament handling where winding tension and rotational speed must remain within tight bounds. Some applications rely on centrifugation-like separation steps or surface finishing, where the rotation profile influences final surface properties. There are also test and conditioning steps—rotational stress tests, balancing checks, material conditioning by controlled rotation, or process stabilization steps—that benefit from repeatable motion sequences.
When spinning steps are automated, the system typically includes:
In this context, “Automatica” usually signals that the system uses closed-loop control (and often recipe management) rather than purely open-loop spinning. A closed-loop system adjusts motor actuation based on measured feedback to follow a target rotational profile—such as ramp-up to speed, hold/dwell at speed for a specified time, and ramp-down under controlled conditions. During evaluation, the core question becomes: does the automation stabilize the process in a way that reduces variation and supports predictable quality and safety behavior? If the system only spins with nominal settings but lacks strong feedback-based control and robust stability handling, it may underperform when the real process deviates from ideal assumptions.
Industrial efficiency is often discussed in terms of OEE (Overall Equipment Effectiveness), and Spin Automatica affects multiple OEE components:
It is also important to recognize that efficiency gains may come indirectly. For example, good recipe and changeover design can reduce operator burden and mistakes. Similarly, integration that provides clear status signals to the line controller can prevent unnecessary waiting or mis-sequenced operations. In many plants, the biggest efficiency losses come from “soft failures”: unclear alarms, ambiguous line handshake logic, and slow commissioning due to missing interface definitions. Spin Automatica matters because it can either eliminate these soft failures through disciplined engineering—or introduce them if the system is under-specified or poorly integrated.
When comparing Spin Automatica solutions, several categories often determine whether the system becomes a reliable production asset or a recurring maintenance burden. While each project has unique requirements, these criteria frequently appear at the top of successful procurement checklists.
These criteria should influence your requirement specification and acceptance test plan. If you only ask for “the lowest price” or “a system that can reach speed X,” you risk selecting a solution that looks good on paper but fails when integrated into your actual process conditions.
Since you asked for price and supplier details, one important clarification is necessary: without explicit pricing figures or vendor names provided in your input, this guide does not invent numbers or claim specific vendor performance. Instead, it provides a structured approach you can use to obtain comparable quotes. In industrial procurement, pricing varies widely based on duty cycle, safety category, instrumentation density, integration scope, and whether the supplier includes commissioning, training, and acceptance testing in their offer.
To discuss cost realistically with suppliers, ask for itemized quotations that separate mechanical, electrical, software, safety, integration, and testing scope. This allows cost drivers to be seen clearly rather than hidden inside a single lump sum.
Ask suppliers to break down cost in categories such as:
One practical procurement technique is to standardize assumptions early. If you require multiple comparable bids, you must standardize the spin cycle profile, expected operating cycle time, and fault recovery behaviors. Otherwise, suppliers may quote different responsibilities or test targets, and the “price comparison” becomes meaningless because the scope is not comparable.
Supplier credibility is typically validated not through sales assurances but through deliverables: engineering documentation quality, test plans, acceptance criteria clarity, and evidence from prior projects. A strong supplier for Spin Automatica typically provides:
To make this more concrete, suppliers should be able to show how the system behaves under both normal and abnormal conditions. For abnormal conditions, you should ask for specific examples: what happens when sensor feedback fails, when load changes suddenly, or when a guard door opens mid-cycle. The best suppliers do not just say “safety stops the machine”; they demonstrate what state transitions occur and how quickly the system responds.
Although “spinning” can refer to multiple manufacturing tasks, engineering evaluation often converges on common fundamentals: how the system behaves under load, how quickly it transitions between recipes, how it handles variability in real materials, and how it ensures safe operation during faults or abnormal events. Below are examples of how Spin Automatica-like systems are commonly applied.
In each scenario, the engineering objective is the same: stabilize the process first, then make the system maintainable and safe across the entire lifecycle. That includes supporting fast fault recovery and minimizing downtime associated with commissioning and changeovers.
Use the following comparison table after you have a draft requirement specification, not before. It is designed to help you compare proposals from different suppliers on equal terms. If a supplier cannot provide evidence for the “evidence to request” column, it is a signal that the proposal may not meet your risk and acceptance expectations.
| Category | What to Require | What “Good” Looks Like | Evidence to Request |
|---|---|---|---|
| Target spin profile | Defined ramp-up, steady-state speed, dwell, ramp-down | Profiles remain consistent across batches and cycles | Test results, control screenshots, or parameter trace logs |
| Feedback and control | Encoder/tachometer feedback and closed-loop control | Low overshoot and stable speed under expected load | Control loop documentation and measured stability curves |
| Control tuning method | Defined approach to loop tuning and commissioning procedure | Documented tuning yields stable behavior across the load range | Commissioning procedure, tuning parameters, and acceptance results |
| Safety requirements | Guarding, E-stop, interlocks, safe stop logic | Safety behavior deterministic and validated | Safety documentation and FAT/SAT safety test records |
| Integration scope | PLC/HMI interfaces and line sequencing behavior | Clear handshake logic, no ambiguous timing dependencies | Interface control documents (ICDs) and wiring/pinout details |
| Recipe management | Named recipes with audit trail and controlled changeover | Controlled changeover with validation before production | Sample HMI screens and recipe validation workflow |
| Diagnostics | Fault codes, event history, sensor health status | Technicians can trace root cause quickly | Fault code list, event history examples, diagnostic screenshots |
| Data logging | Recorded speed/torque/vibration/temperature for traceability (as needed) | Data available to correlate process parameters and quality outcomes | Sample data logs, sampling rate documentation, historian integration details |
| Spare parts and service | Defined maintenance intervals and recommended spares | Planned service reduces unplanned stoppages | Spare parts list, service SLA, lead time estimates |
| Commissioning timeline | Detailed FAT/SAT schedule and acceptance criteria | Startup risk minimized with staged testing | Commissioning plan, acceptance checklists, FAT/SAT scripts |
| Change management | Version control for control software and recipe sets | Clear process for software updates without unexpected behavior | Change control process, versioning strategy, documentation for upgrades |
This step-by-step guide reflects how many engineering procurement teams structure evaluation. The order matters: you want requirements locked before performance testing, and performance testing locked before procurement decisions. If you start with procurement without well-defined acceptance criteria, you often end up negotiating after the fact—during commissioning—when time and cost constraints intensify.
One additional practice that can reduce risk is to schedule a “controls interface review” meeting before FAT. In this meeting, you and the supplier walk through handshake logic, alarm severity mapping, and how the line controller reacts to faults. This prevents the common situation where the machine can run alone in FAT but fails to behave properly when integrated.
To keep expectations realistic and technically grounded, consider the conditions below before commissioning a Spin Automatica system. Each of these categories can influence whether the system meets performance targets or produces unexpected issues.
Even when a supplier claims the control system is “robust,” that robustness depends on mechanical stability and correct sensing strategy. A mispositioned sensor or inadequate coupling alignment can cause feedback noise or bias, leading to inconsistent speed and increased wear on mechanical components.
In automation procurement, many organizations rely on internationally recognized frameworks to reduce risk and standardize safety and documentation practices. For safety-critical machinery design and validation, many manufacturers align their work with ISO 12100 (safety of machinery—general principles for design) and IEC 62061 / ISO 13849-1 (functional safety for safety-related control systems). For quality management and documentation governance in production systems, ISO 9001 provides a governance structure for documentation, change control, and continuous improvement.
These standards are not meant to replace your project-specific risk assessment; rather, they provide structured approaches and vocabulary for designing, validating, and documenting safety and quality processes. That matters because Spin Automatica systems often involve high energy motion components, hazardous rotating parts, and complex fault conditions. Using recognized frameworks ensures safety requirements are not left ambiguous or handled informally.
For the “evidence-based” part: you should expect test evidence tied to acceptance criteria, not simply a demonstration. For example, rather than “we stopped safely,” you should require a documented demonstration showing safe stop behavior under defined conditions: door open mid-cycle, emergency stop during steady state, overspeed simulation if possible, and sensor fault reaction logic. Your acceptance criteria should be measurable and reproducible.
To make your evaluation actionable, it helps to understand what “good control” means for rotational automation. In many spinning applications, control quality can be judged by several measurable behaviors:
When suppliers provide FAT/SAT traces, focus on these characteristics. You may ask suppliers to provide multiple traces under representative loads to demonstrate repeatability. If they provide only “best case” traces, request additional runs.
Another key aspect is controller tuning strategy and robustness. A controller tuned only for one nominal condition may perform poorly when the actual load differs. Therefore, it is advisable to require a documented tuning procedure and to ask how the supplier ensures stable control across expected load ranges. If your process includes dynamic load changes mid-cycle (e.g., clamp engaging, material wetting, or viscosity changes), demand that these scenarios be part of the evidence.
Spin control quality is heavily influenced by sensing. Consider what sensors are used and how reliably they measure what the controller needs to know. Common elements include:
During evaluation, ask how sensor health is monitored and how the system reacts to sensor faults. For example:
A system that fails with generic error codes makes troubleshooting difficult. A system that logs “encoder A signal lost for 200 ms” or “vibration sensor out of range” enables faster recovery.
Safety engineering is central for Spin Automatica because the hazard is not hypothetical—high-speed rotating components can cause serious injury if access is allowed or if the machine does not stop predictably.
When you evaluate safety, consider both functional safety and the practical reality of safe stopping behavior. You should require:
It is also important to verify that safety design aligns with actual facility processes. For example, if maintenance access requires a lockout/tagout procedure, the safety system design should support it and the operation manual should clearly instruct technicians on safe ways to isolate energy.
Even if the spin controller is excellent, integration can undermine the results. Many commissioning delays happen not because the machine cannot spin, but because it cannot coordinate with the line controller reliably.
Integration evaluation should include:
As part of proposal evaluation, you can ask suppliers for interface control documents (ICDs), signal list with meaning, and examples of typical operational sequences (start-to-finish). If they provide only generic diagrams, request more detail.
Maintainability is a major efficiency driver. Two systems with the same uptime potential can differ significantly in actual downtime due to diagnostic clarity and maintenance ease.
When evaluating maintainability, consider:
A practical procurement approach is to ask suppliers to estimate mean time to repair (MTTR) for typical fault categories and to describe the troubleshooting workflow. If the supplier can’t provide any meaningful diagnostic guidance, you should factor that into TCO and acceptance risk.
Spin Automatica systems often include recipe management. Recipes define speed profiles, ramp rates, dwell times, and sometimes safety thresholds or process-specific parameters.
Efficient operation depends on how recipes are managed. When evaluating recipe management, require:
Recipe quality is part of efficiency. Poor recipe management increases training burden, introduces errors, and creates inconsistent production results. Good recipe management supports disciplined production and reduces the need for manual interventions.
Commissioning can be the largest hidden cost in automation projects. To avoid surprises, ensure suppliers provide a structured commissioning strategy with staged testing and clear acceptance criteria.
A typical commissioning strategy includes:
Demand that the supplier define responsibilities clearly: which tasks are done by the supplier, which by your team, and which are shared. Ambiguity here is a common reason for schedule slips.
A major reason projects struggle at acceptance time is that acceptance criteria are vague. “Good performance” is not measurable. You should require acceptance criteria that are tied to what matters: speed profile stability, dwell time accuracy, fault recovery behavior, and safety response times or state transitions.
Examples of measurable acceptance criteria you might request (adapt these to your process):
When you request these criteria from suppliers, you reduce the likelihood of disputes later. You also improve the quality of the supplier’s FAT/SAT evidence.
When you compare suppliers, standardization is what makes comparisons fair. If one supplier tests the system with a simplified load model and another tests under realistic representative loads, the “best supplier” may not be the one with the lowest price. Instead, the correct approach is to standardize:
Once you standardize, you can compare suppliers using evidence: measured speed traces, fault logs, and documented acceptance testing results.
Spin Automatica typically refers to an automated spinning/rotational process system that uses closed-loop motion control and sensors to keep a target speed and cycle profile consistent. In practice, it coordinates mechanical actuation, sensing, and control logic so the process repeats reliably across batches and shifts.
Compare them using equal scope definitions: target spin profile, control and sensor feedback method, safety design approach, integration boundaries, diagnostics quality, and commissioning acceptance criteria. Request itemized quotations and evidence from FAT/SAT results rather than relying on general performance statements. Use a consistent requirements document and require suppliers to show measured traces for speed tracking, settling, and safety behavior.
Not fully. Purchase price is only part of TCO. Maintenance intervals, spare parts availability, diagnostic tooling quality, commissioning effort, training time, and downtime risk can significantly affect total cost over the system’s operational life. A slightly higher purchase price can reduce downtime and commissioning delays, resulting in lower overall TCO.
Commonly requested documents include interface specifications (ICDs), electrical and control documentation, safety documentation, FAT/SAT test plans and records, maintenance manuals, and training materials. The exact list should match your procurement requirements and internal standards. If your line controller requires specific tag mapping or timing behavior, insist on ICD-level detail during proposal stage.
Key items include safe stop behavior, response to interlock conditions (e.g., guard/door status), overspeed or sensor fault reactions, and emergency stop logic. Acceptance should be tied to measurable criteria defined in advance, and evidence should be documented through FAT/SAT safety test records.
Often yes, but integration must be defined upfront: timing handshake logic, control system communication protocols, and how the machine reports status/faults to the line controller. Ambiguity here is a common cause of delayed commissioning. Require interface control documents and validate handshake sequences during FAT and rehearsal during SAT.
Include the cycle profile (ramp/speed/dwell), expected load ranges, quality-relevant parameters, safety constraints, operator workflow expectations, and interface requirements. The clearer the specification, the more comparable suppliers’ quotes and test results will be. Also specify diagnostics and data logging requirements if traceability or root-cause analysis is important to your quality and maintenance processes.
Yes—mismatched integration assumptions, unclear responsibility for interface wiring, insufficient definition of acceptance criteria, and underestimating training time. Other common pitfalls include inadequate testing under representative load conditions and missing evidence of safety behavior for abnormal scenarios. Using staged FAT and clearly documented SAT acceptance helps reduce these risks.
Then your evaluation should require stability testing across the full load range you expect. If the controller is tuned only for a nominal condition, speed accuracy and settling behavior may degrade when load changes. Ask suppliers how they validate performance under variable load and what tuning or calibration steps are included.
Not necessarily for every application, but it can significantly improve maintenance effectiveness in cases where imbalance, bearing wear, or resonance issues are plausible. If your process is sensitive to mechanical stability or you expect high duty cycles, request vibration monitoring or at least a stability indicator that can support predictive maintenance and early fault detection.
Spin Automatica systems deliver value when they are evaluated through measurable, engineering-based criteria: stable control of rotational profiles, well-defined safety functions, predictable diagnostics, and an integration scope that matches the reality of your production line. Price matters, but price only becomes meaningful when scope, acceptance criteria, and evidence requirements are standardized across bids.
This guide avoids unverifiable claims and does not invent supplier or price details. Your practical next step is to convert your process needs into a structured requirements document, including spin cycle profiles, integration expectations, safety scenarios to test, diagnostics/data logging requirements, and measurable FAT/SAT acceptance criteria. Then request comparable, itemized proposals that include evidence from FAT/SAT runs under representative conditions.
If you share your target application (what is being spun, expected cycle time, material behavior, and the integration environment—PLC brand, safety system context, and line handshake requirements), the evaluation framework can be tailored further. You can refine the comparison table fields and produce a tighter requirement checklist aligned to your real constraints while keeping the procurement objective and evidence-based evaluation approach intact.
Striking the Perfect Balance: Navigating Premiums and Out-of-Pocket Expenses in Senior Insurance Plans
Explore the Tranquil Bliss of Idyllic Rural Retreats
How to Make Lasting Memories at Disneyland Attractions
Affordable Phones and Plans for Seniors
Affordable Full Mouth Dental Implants Near You
Unlock the Top Kept Secrets to Finding Your Ideal Dentist for Flawless Dental Implant Results!
Discovering Springdale Estates
The Guide to Car Trading
Affordable Cell Phones Without Plans
Unveiling Grunig & Hunt's PR Models
This article explores the seminal work of Grunig & Hunt in developing models of public relations. The Grunig & Hunt models, fundamental to understanding PR theory, provide insight into the strategic approaches and methodologies utilized in the field. Each model offers a distinctive perspective on communication and engagement strategies, relevant to both academic discussions and practical applications.
Understanding Attimo Family Office
Attimo Family Office represents a new trend in wealth management services, designed to serve high-net-worth families with personalized attention and expertise. These offices provide tailored financial, investment, and lifestyle management to ensure good wealth preservation and growth. Emphasizing trust, discretion, and bespoke solutions, they cater to the distinct needs of affluent families.
Navigating Attimo Family Office Services
Attimo Family Office is a specialized financial service provider dedicated to managing the complex financial needs of affluent families. By offering personalized advice tailored to each family's unique circumstances, they help in safeguarding wealth across generations. The concept of a family office has been increasingly embraced by high-net-worth individuals seeking tailored investment strategies, tax planning, and legacy management.
Understanding Grunig & Hunt's PR Models
This article delves into the renowned Grunig & Hunt models of public relations, highlighting their significant contribution to the field of strategic communication. Developed by James E. Grunig and Todd Hunt, these models have guided PR practitioners in understanding and executing effective public relations strategies. This guide aims to elaborate on each model, explore their application in real-world scenarios, and underscore their relevance in contemporary PR practices.
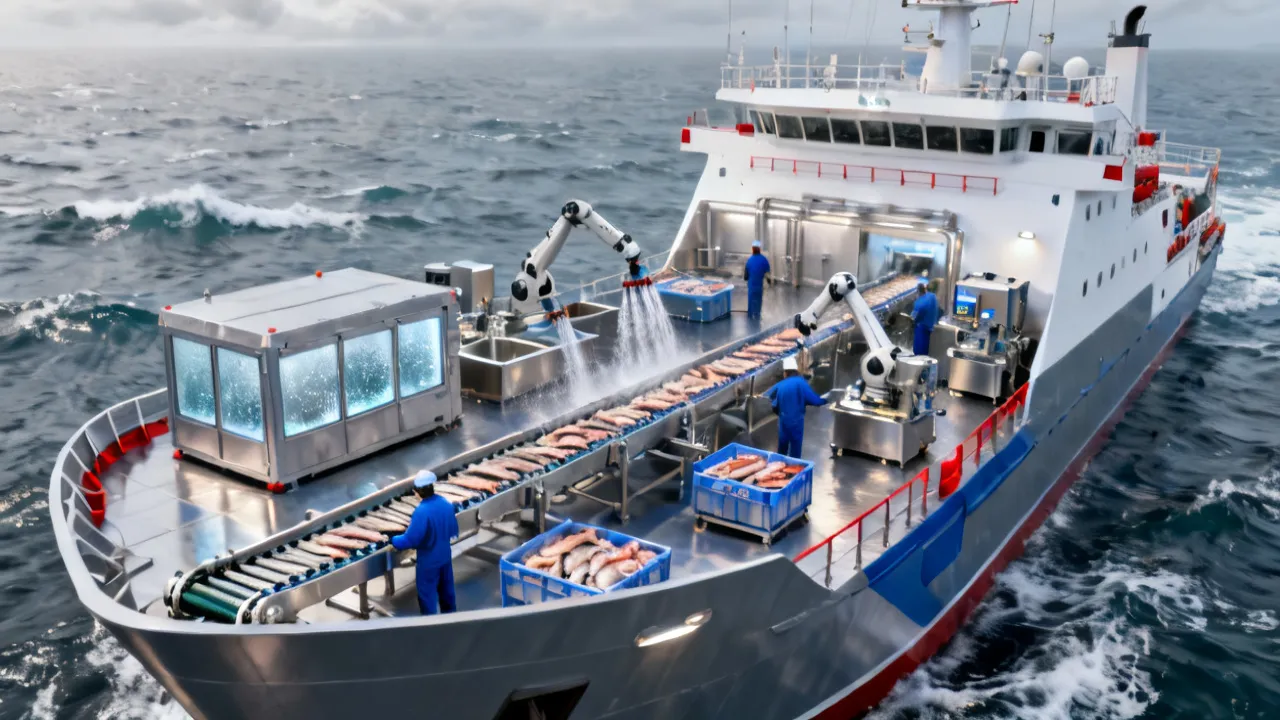
Unveiling the Optimar Rae
An in-depth exploration of the Optimar Rae, a frontrunner in seafood processing. Known for its advanced technology and efficiency, the Optimar Rae plays a pivotal role in modernizing seafood operations. This article delves into its significance, examining how it enhances productivity while maintaining environmental standards, marking a new era in maritime industry advancements.
Mastering Employee Retention Strategies
This article delves into the essential role of an Employee Retention Consultant. Employee retention is crucial for maintaining a competitive edge and fostering a positive work environment. Professional consultants help organizations in developing tailored retention strategies to reduce turnover, increase job satisfaction, and enhance overall productivity. Explore expert insights, strategies, and FAQs in employee retention.